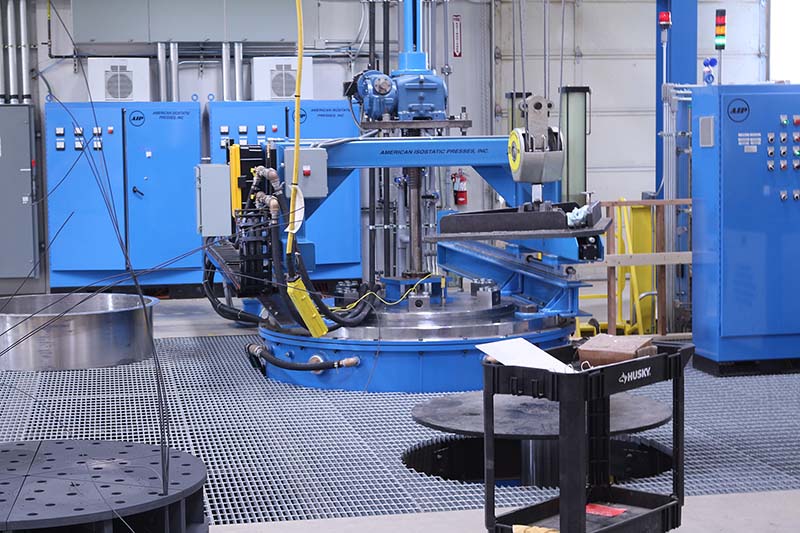
How Does Hot Isostatic Pressing Work?
Hot Isostatic Pressing, commonly known as HIP, is a manufacturing process that combines high temperature with uniform gas pressure inside a sealed pressure vessel.
The process is used to reduce internal porosity, improve material density and enhance the reliability of suitable cast, sintered, ceramic and metal additively manufactured components.
Table of Contents
Unlike mechanical pressing, HIP does not apply force from only one direction. Pressurised gas surrounds the component and applies pressure uniformly across all exposed surfaces.
Explore Lodestar 3D’s Hot Isostatic Pressing technology solutions for laboratory, scale-up and production requirements.
What Happens During the HIP Process?
A typical hot isostatic pressing cycle involves the following stages.
1. Component Preparation
The component or material is cleaned and prepared before processing.
Castings and metal 3D printed parts may be processed directly when their outer surfaces are sufficiently sealed. Powders may need to be placed inside an evacuated and sealed container before consolidation.
2. Loading the HIP System
The component is placed inside the furnace’s usable hot zone.
The hot-zone diameter and length must be large enough to accommodate the component, tooling or production batch. This makes chamber size an important factor when selecting a HIP system.
For laboratory research, the AIP6-30H Laboratory Hot Isostatic Press provides a compact platform for developing and testing HIP cycles.
3. Closing and Pressurising the Vessel
The pressure vessel is securely closed, and an inert process gas is introduced.
Argon is commonly used because it is chemically inert under many HIP processing conditions. The gas is gradually pressurised according to the selected process cycle.
4. Heating the Component
An internal furnace raises the component to the required processing temperature.
The temperature is selected according to the material and desired result. The material is heated sufficiently to support deformation and diffusion without being melted.
5. Holding at Temperature and Pressure
Once the target temperature and pressure are reached, the system holds these conditions for a defined period.
During this stage, pressure pushes the internal surfaces of pores together. Heat allows the surrounding material to deform and bond, helping reduce voids and improve density.
The final result depends on:
- Material type
- Starting density
- Component dimensions
- Temperature
- Pressure
- Holding time
- Initial defect condition
6. Cooling and Depressurisation
After the holding period, the system begins a controlled cooling and depressurisation sequence.
Pressure and temperature must be reduced safely before the vessel can be opened.
7. Component Inspection
The processed component is removed and inspected.
Inspection may include density measurement, dimensional checks, non-destructive testing, mechanical testing or microstructure evaluation.
How Does HIP Reduce Internal Porosity?
Internal porosity consists of small pores or voids trapped within a manufactured component.
During HIP, elevated temperature makes the material more responsive to pressure. Uniform gas pressure acts on the component from every direction and pushes the pore surfaces together.
This combination can help close suitable internal voids and improve structural consistency.
However, HIP cannot correct every defect. Surface-connected pores, contamination, major cracks and dimensional problems may require other manufacturing or repair methods.
What Components Can Be HIP Processed?
Internal porosity consists of small pores or voids trapped within a manufactured component.
During HIP, elevated temperature makes the material more responsive to pressure. Uniform gas pressure acts on the component from every direction and pushes the pore surfaces together.
This combination can help close suitable internal voids and improve structural consistency.
However, HIP cannot correct every defect. Surface-connected pores, contamination, major cracks and dimensional problems may require other manufacturing or repair methods.
What Components Can Be HIP Processed?
Hot isostatic pressing is commonly considered for:
- Metal castings
- Metal 3D printed components
- Powder metallurgy parts
- Sintered components
- Advanced ceramics
- Encapsulated powders
- Diffusion-bonded assemblies
Learn more about HIP applications across industrial manufacturing and how the process supports different component-development stages.
Main Benefits of Hot Isostatic Pressing
HIP can provide several benefits when the material and cycle are correctly matched:
- Reduced internal porosity
- Improved material density
- Better structural consistency
- Enhanced fatigue performance
- Improved component reliability
- Lower rejection and scrap risk
- Support for complex component shapes
The exact improvement varies according to the component and processing conditions
How to Choose the Right HIP System
The appropriate HIP system should be selected according to:
- Component dimensions
- Required hot-zone size
- Operating pressure
- Furnace temperature
- Material type
- Batch capacity
- Research or production volume
- Future scale-up requirements
Lodestar 3D supports the evaluation of AIP hot isostatic press systems for laboratory research, sample scale-up and production processing.
Conclusion
Hot Isostatic Pressing works by applying high temperature and uniform gas pressure to a component inside a sealed pressure vessel.
A typical cycle includes preparation, loading, gas pressurisation, heating, holding, cooling, depressurisation and inspection. The combined effect of temperature, pressure and time helps reduce internal porosity and improve material density.
Need help selecting the right hot-zone size, pressure or production capacity? Talk to a Lodestar 3D HIP expert about your requirements.
FAQ's
What gas is used in hot isostatic pressing?
Argon is commonly used because it is inert and generally does not react with the processed material.
Does HIP melt the component?
No. Conventional HIP normally operates below the material’s melting temperature.
Can HIP remove all internal defects?
No. HIP can reduce suitable sealed internal porosity but may not repair surface-connected pores, contamination or major cracks.
Is HIP suitable for metal 3D printed parts?
Yes. HIP is commonly evaluated as a post-processing method for suitable metal additively manufactured components.
How can Lodestar 3D help?
Lodestar 3D can assess your material, component size, temperature, pressure and production requirements to help identify a suitable AIP HIP system.